
After a hanger shot blasting machine, surface quality is determined by three separate checks: the visual cleanliness grade to ISO 8501-1 (Sa 1–Sa 3), the surface profile to ISO 8503, and invisible contaminants (soluble salts and dust) to ISO 8502. Until all three are checked, no surface is ready for coating.
This guide explains each check, the machine’s effect, and what buyers in Poland, Romania and Austria should specify.
What Does Surface Quality After Shot Blasting Mean?
Surface quality consists of three independently measured elements:
- Cleanliness grade: how much rust, mill scale and old paint remains.
- Surface profile (roughness): the peak-to-valley depth the abrasive creates; the coating keys into it.
- Contaminant level: soluble salts and dust the eye cannot detect.
| Common MistakeSa 2½ is a cleanliness grade, not a roughness value. Roughness is measured separately in microns (µm) under ISO 8503. |
How Is Cleanliness Measured After a Hanger Shot Blasting Machine?
Cleanliness is judged visually: the part leaving the hanger shot blasting machine is compared with the ISO 8501-1 photographic references under adequate light. International projects often ask for AMPP (formerly SSPC/NACE) equivalents:
| ISO 8501-1 | AMPP / SSPC | Description |
|---|---|---|
| Sa 1 | SP 7 | Light (brush-off) blast cleaning |
| Sa 2 | SP 6 | Thorough (commercial) blast cleaning |
| Sa 2½ | SP 10 | Very thorough (near-white metal) |
| Sa 3 | SP 5 | Visually clean steel (white metal) |
Should You Target Sa 2½ or Sa 3?
- Sa 2½ – Pro: accepted by most industrial coating systems; cycle time and abrasive use stay reasonable. Con: light shadows or staining may remain.
- Sa 3 – Pro: no residue accepted; suits tank linings and aggressive environments. Con: longer cycles, higher energy and abrasive cost.
Unless Sa 3 is specified, Sa 2½ is the best balance of cost and performance.
How Is Surface Profile Measured on a Hanger Type Shot Blasting Machine?
Three common methods are used for profile (roughness):
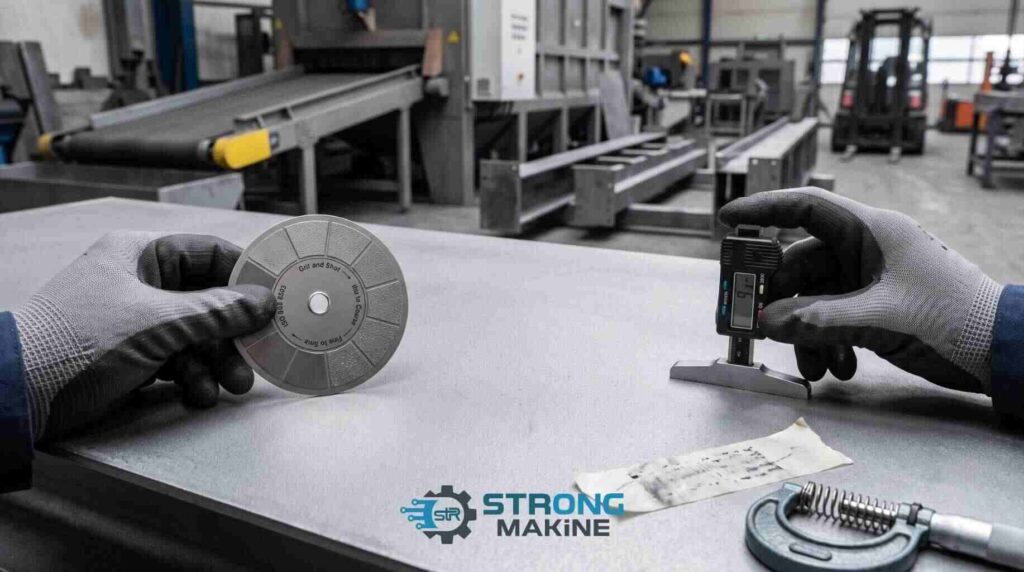
- Comparator disc (ISO 8503-1/-2): separate discs for grit (G) and shot (S). Fast, but gives a Fine, Medium or Coarse class rather than a number.
- Replica tape (ISO 8503-5): foam tape is burnished onto the surface and read with a spring micrometer. The tape can be archived as a physical record.
- Digital depth gauge (ASTM D4417 Method B): a probe reads peak-to-valley depth directly; the fastest option for multi-point checks.
Does Shot or Grit Create a Deeper Profile?
Angular grit creates a deeper profile; round shot gives a shallower, smoother surface. ISO 8503-1 comparator classes are approximately:
| Class | Grit (G) | Shot (S) |
|---|---|---|
| Fine | 25–60 µm | 25–40 µm |
| Medium | 60–100 µm | 40–70 µm |
| Coarse | 100–150 µm | 70–100 µm |
The binding target is in the coating data sheet (TDS). Too shallow and the coating cannot key in; too deep and peaks protrude through the film.
How Are Invisible Contaminants Checked?
- Soluble salts: the Bresle method (ISO 8502-6) extracts a water sample, conductivity is measured (ISO 8502-9) and the result is reported in mg/m².
- Dust: adhesive tape is pressed onto the surface and rated for quantity and particle size under ISO 8502-3.
- Climate: ISO 8502-4 covers humidity and dew point. A common rule is that steel must be at least 3 °C above dew point.
What Should Buyers in Poland, Romania and Austria Check?
These ISO standards are adopted as European standards, so projects in Poland (PN-EN ISO), Romania (SR EN ISO) and Austria (ÖNORM EN ISO) use the same references. For painted steel structures, EN 1090-2 refers to the ISO 8501 series and EN ISO 12944 for surface preparation.
- Confirm the required Sa grade and profile range in the coating TDS before choosing abrasive.
- Ask for a blasting report that includes cleanliness, profile and, where required, salt and dust results.
- Check that the hanger shot blasting machine suits your largest part and hook load.
How Does the Hanger Shot Blasting Machine Affect the Result?
In the hanger shot blasting machine process, the part rotates on the hook so abrasive from the turbines reaches every face. Key parameters:
- Hook rotation and loading: parts hung too closely shadow each other and lower the grade.
- Turbine count and flow: larger baskets need more turbines for uniform coverage.
- Blast time: cycles that are too short do not reach the target Sa grade.
- Abrasive mix: the separator removes dust and broken grains, keeping the profile stable.
- Dust collection: weak filtration leaves dust and degrades the ISO 8502-3 result.
Strong Makine’s AK series hanger type shot blasting machine models control these parameters with manganese steel lined cabins, automatic abrasive recovery and a Jet-Pulse filter unit:
| Feature | AK-0 | AK-1 | AK-2 | AK-3 | AK-4 | AK-5 |
|---|---|---|---|---|---|---|
| Basket diameter (mm) | 900 | 1200 | 1200 | 1500 | 2000 | 2250 |
| Basket height (mm) | 1100 | 1200 | 1500 | 1600 | 2200 | 3000 |
| Hook capacity (t – qty) | 0.5 – 2 | 1.5 – 2 | 2 – 2 | 2 – 2 | 5 – 1 | 7.5 – 1 |
| Turbines | 2 | 2 | 2 | 2 | 4 | 6 |
| Abrasive flow per turbine (kg/min) | 100 | 190 | 240 | 240 | 190 | 240 |
| Jet-Pulse filter (m²) | 18 | 36 | 36 | 48 | 64 | 100 |
To match a model to your parts, see the Hanger shot blasting machine product page or request a quote.
Frequently Asked Questions – FAQ
How long does a blasted surface stay clean?
Blasted steel is unprotected and flash rusts quickly in moisture. The window depends on humidity and temperature; aim to prime within the same shift.
What is the difference between Rz and Ra?
Ra is an average and can hide isolated deep valleys. Rz uses peak-to-valley heights and is preferred before coating.
Which parts suit a hanger type shot blasting machine?
A hanger shot blasting machine suits castings, welded structures and automotive parts too large or complex to be tumbled.
Is Sa 2½ adequate for every coating system?
No. Sa 2½ suits most industrial systems, but tank linings and some specifications require Sa 3. The coating data sheet decides.
Is the cleanliness grade the same as roughness?
No. The Sa grade states contamination left behind; roughness (µm) states profile depth. They are measured and reported separately.
People Also Ask – PAA
What does Sa 2.5 mean?
It is the ISO 8501-1 “very thorough blast cleaning” grade; only light shadows or staining may remain.
Which instrument measures blasting roughness?
A comparator disc, replica tape with a spring micrometer, or a digital depth gauge.
Is a salt test mandatory after shot blasting?
Not on every project. It is usually specified for seawater, chemical exposure or high corrosivity categories.
| Author: STR Strong Makine Engineering TeamPrepared by the engineering team of STR Strong Makine, founded in 2023 on its founders’ 20 years of surface treatment experience. Methods follow ISO and AMPP standards. Sources: Abrasive blasting (Wikipedia) · Kum püskürtme (Vikipedi) |
If you enjoyed our article titled “How Is Surface Quality Measured After Shot Blasting?“, visit our News page for more content.
Contact us for information about Strong Makina.